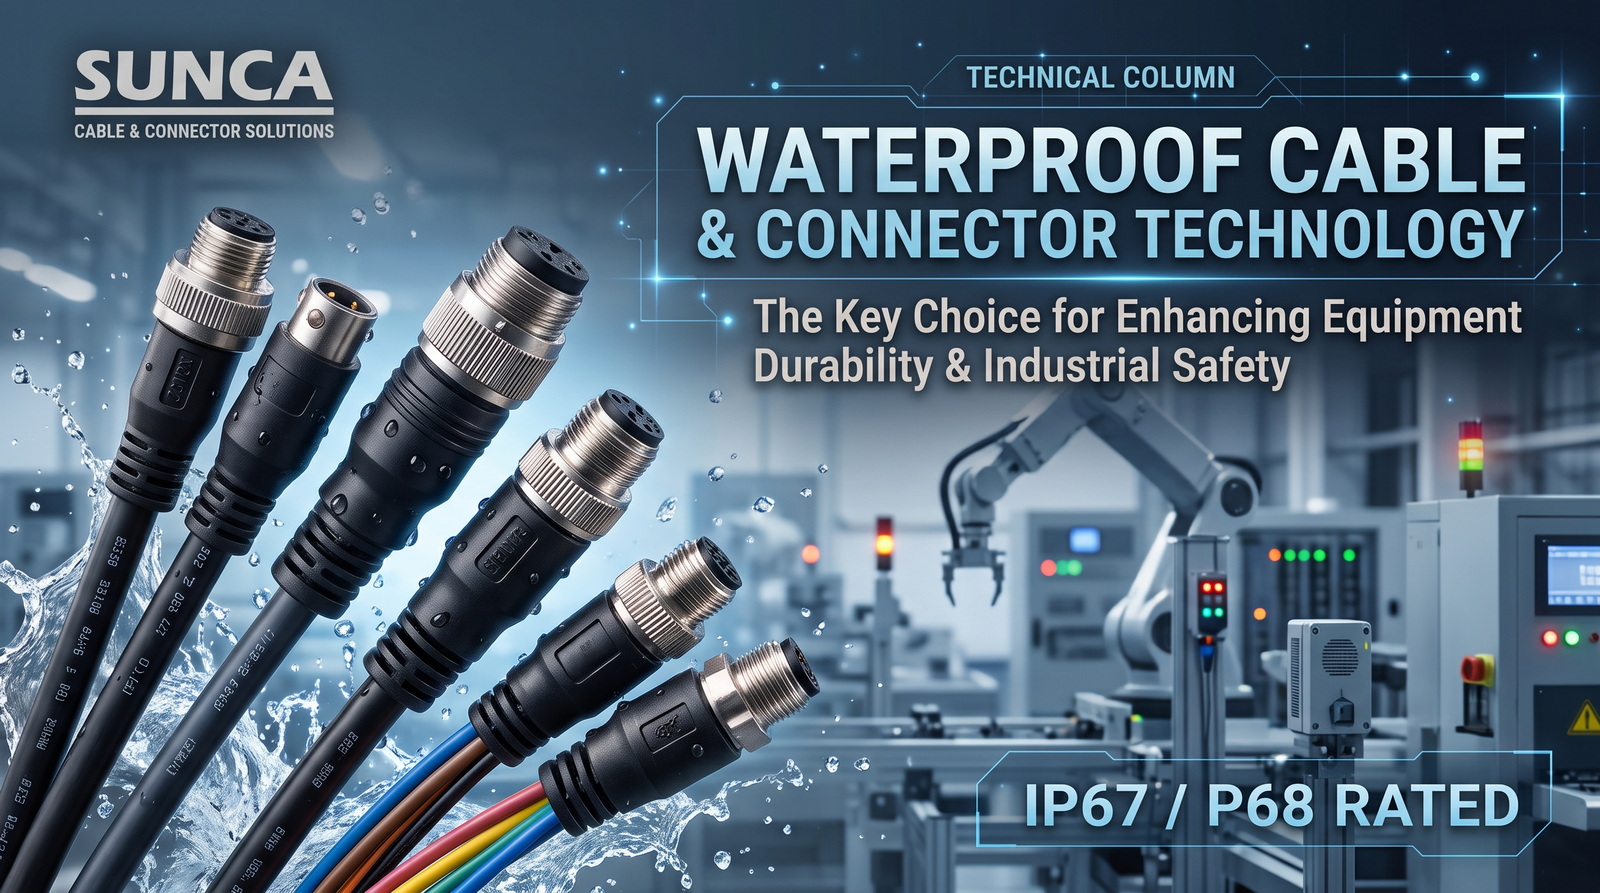
[TECHNICAL COLUMN] Waterproof Cable & Connector Technology: The Key Choice for Enhancing Equipment Durability & Industrial Safety
Why Do Modern Industrial and Electronic Devices Need High-Spec “Waterproof Cables”?
In the realm of modern industry and high-end electronic devices, environmental variables are often the biggest test of hardware lifespan. Whether in food processing plants with high humidity and corrosion risks, outdoor equipment exposed to the elements, or medical and automotive environments requiring strict protection, traditional cables are highly susceptible to moisture intrusion, leading to short circuits, signal attenuation, or even equipment damage.
At this point, waterproof cables with high IP ratings (e.g., IP67, IP68) play a crucial role. They not only effectively block the intrusion of moisture, dust, and chemicals but also serve as the core defense line to ensure stable system operation, reduce maintenance costs, and enhance overall equipment durability.
SUNCA Waterproof Cable & Connector Solutions
SUNCA CO., LTD. possesses a profound background in cable research and development, specializing in the design and manufacture of customized waterproof cables. We understand that maintaining high-speed signal integrity in extreme environments is a technical challenge. Therefore, we provide diverse and highly reliable waterproof connection solutions:
-
Industrial-Grade Waterproof Connectors:
Offering M12, M8, and other specifications that comply with international standards. These connectors feature excellent shock resistance and waterproof/dustproof capabilities, perfectly meeting the stringent demands of sensors, actuators, and various industrial equipment.
-
High-Performance Waterproof Cables:
For high-speed data and audio-visual transmission needs, SUNCA offers high-end cables with waterproof designs, including USB 3.0, HDMI, and DisplayPort (DP). Through precise mechanical design and molding technology, we ensure low-latency, lossless signal transmission even in damp environments.
-
Comprehensive Customized Solutions:
Leveraging our professional engineering team, we provide exclusive customization services tailored to clients’ specific application scenarios—from cable material selection and mold development to waterproof structural design (such as special injection molding), pushing product durability to the limit.
Four Core Application Areas for Waterproof Cables
SUNCA’s waterproof cable technology has been successfully introduced into multiple key industries, providing the most solid hardware backing for our clients:
-
Industrial Automation & Smart Manufacturing:
In factory environments filled with oil, moisture, and strong vibrations, waterproof cables ensure error-free data transmission between robotic arms, PLC control systems, and sensors, guaranteeing 24/7 stable production line operation.
-
Outdoor Surveillance & Networking Equipment:
For security cameras (IP Cameras), outdoor base stations, and other devices, waterproof connection technology can withstand heavy rain and extreme weather, significantly extending the service life of equipment in outdoor environments.
-
High-End Medical Equipment:
Medical environments have strict regulations for equipment cleaning and disinfection. Waterproof cables prevent the risk of electrical leakage caused by liquid ingress, ensuring the safe and reliable data transmission of life monitoring instruments and medical imaging equipment.
-
Automotive-Grade Electronic Systems:
Vehicles face drastic temperature changes and moisture intrusion during operation. SUNCA’s automotive-grade cables are suitable for in-vehicle infotainment systems, Advanced Driver Assistance Systems (ADAS), and other applications, comprehensively enhancing the durability and driving safety of vehicle electronic systems.
Choose SUNCA to Inject the Highest Quality and Reliability into Your Equipment
High-quality waterproof cables are not just bridges connecting equipment; they are guarantees of product quality. SUNCA has accumulated rich experience in cable design and manufacturing. Our entire product line implements strict quality control processes and has passed multiple international certifications to meet global market safety requirements.
Whether you need standardized waterproof connectors or customized waterproof cable solutions tailored for specific environments, SUNCA can provide you with the most competitive technical support, helping your enterprise significantly improve equipment performance, extend product lifespan, and stand out in the market.